HILCO Gas Filters/Separators
HILCO Gas Filters/Separators
Gas Filter/ Separators for Industrial Applications
HILCO utilized computational fluid dynamics (CFD) software to optimize performance and provide customers with accurate predictions of equipment pressure loss before units are put into service. This allows end users and sites to accurately program their auto warning systems proactively for drop in installation once the units arrive.
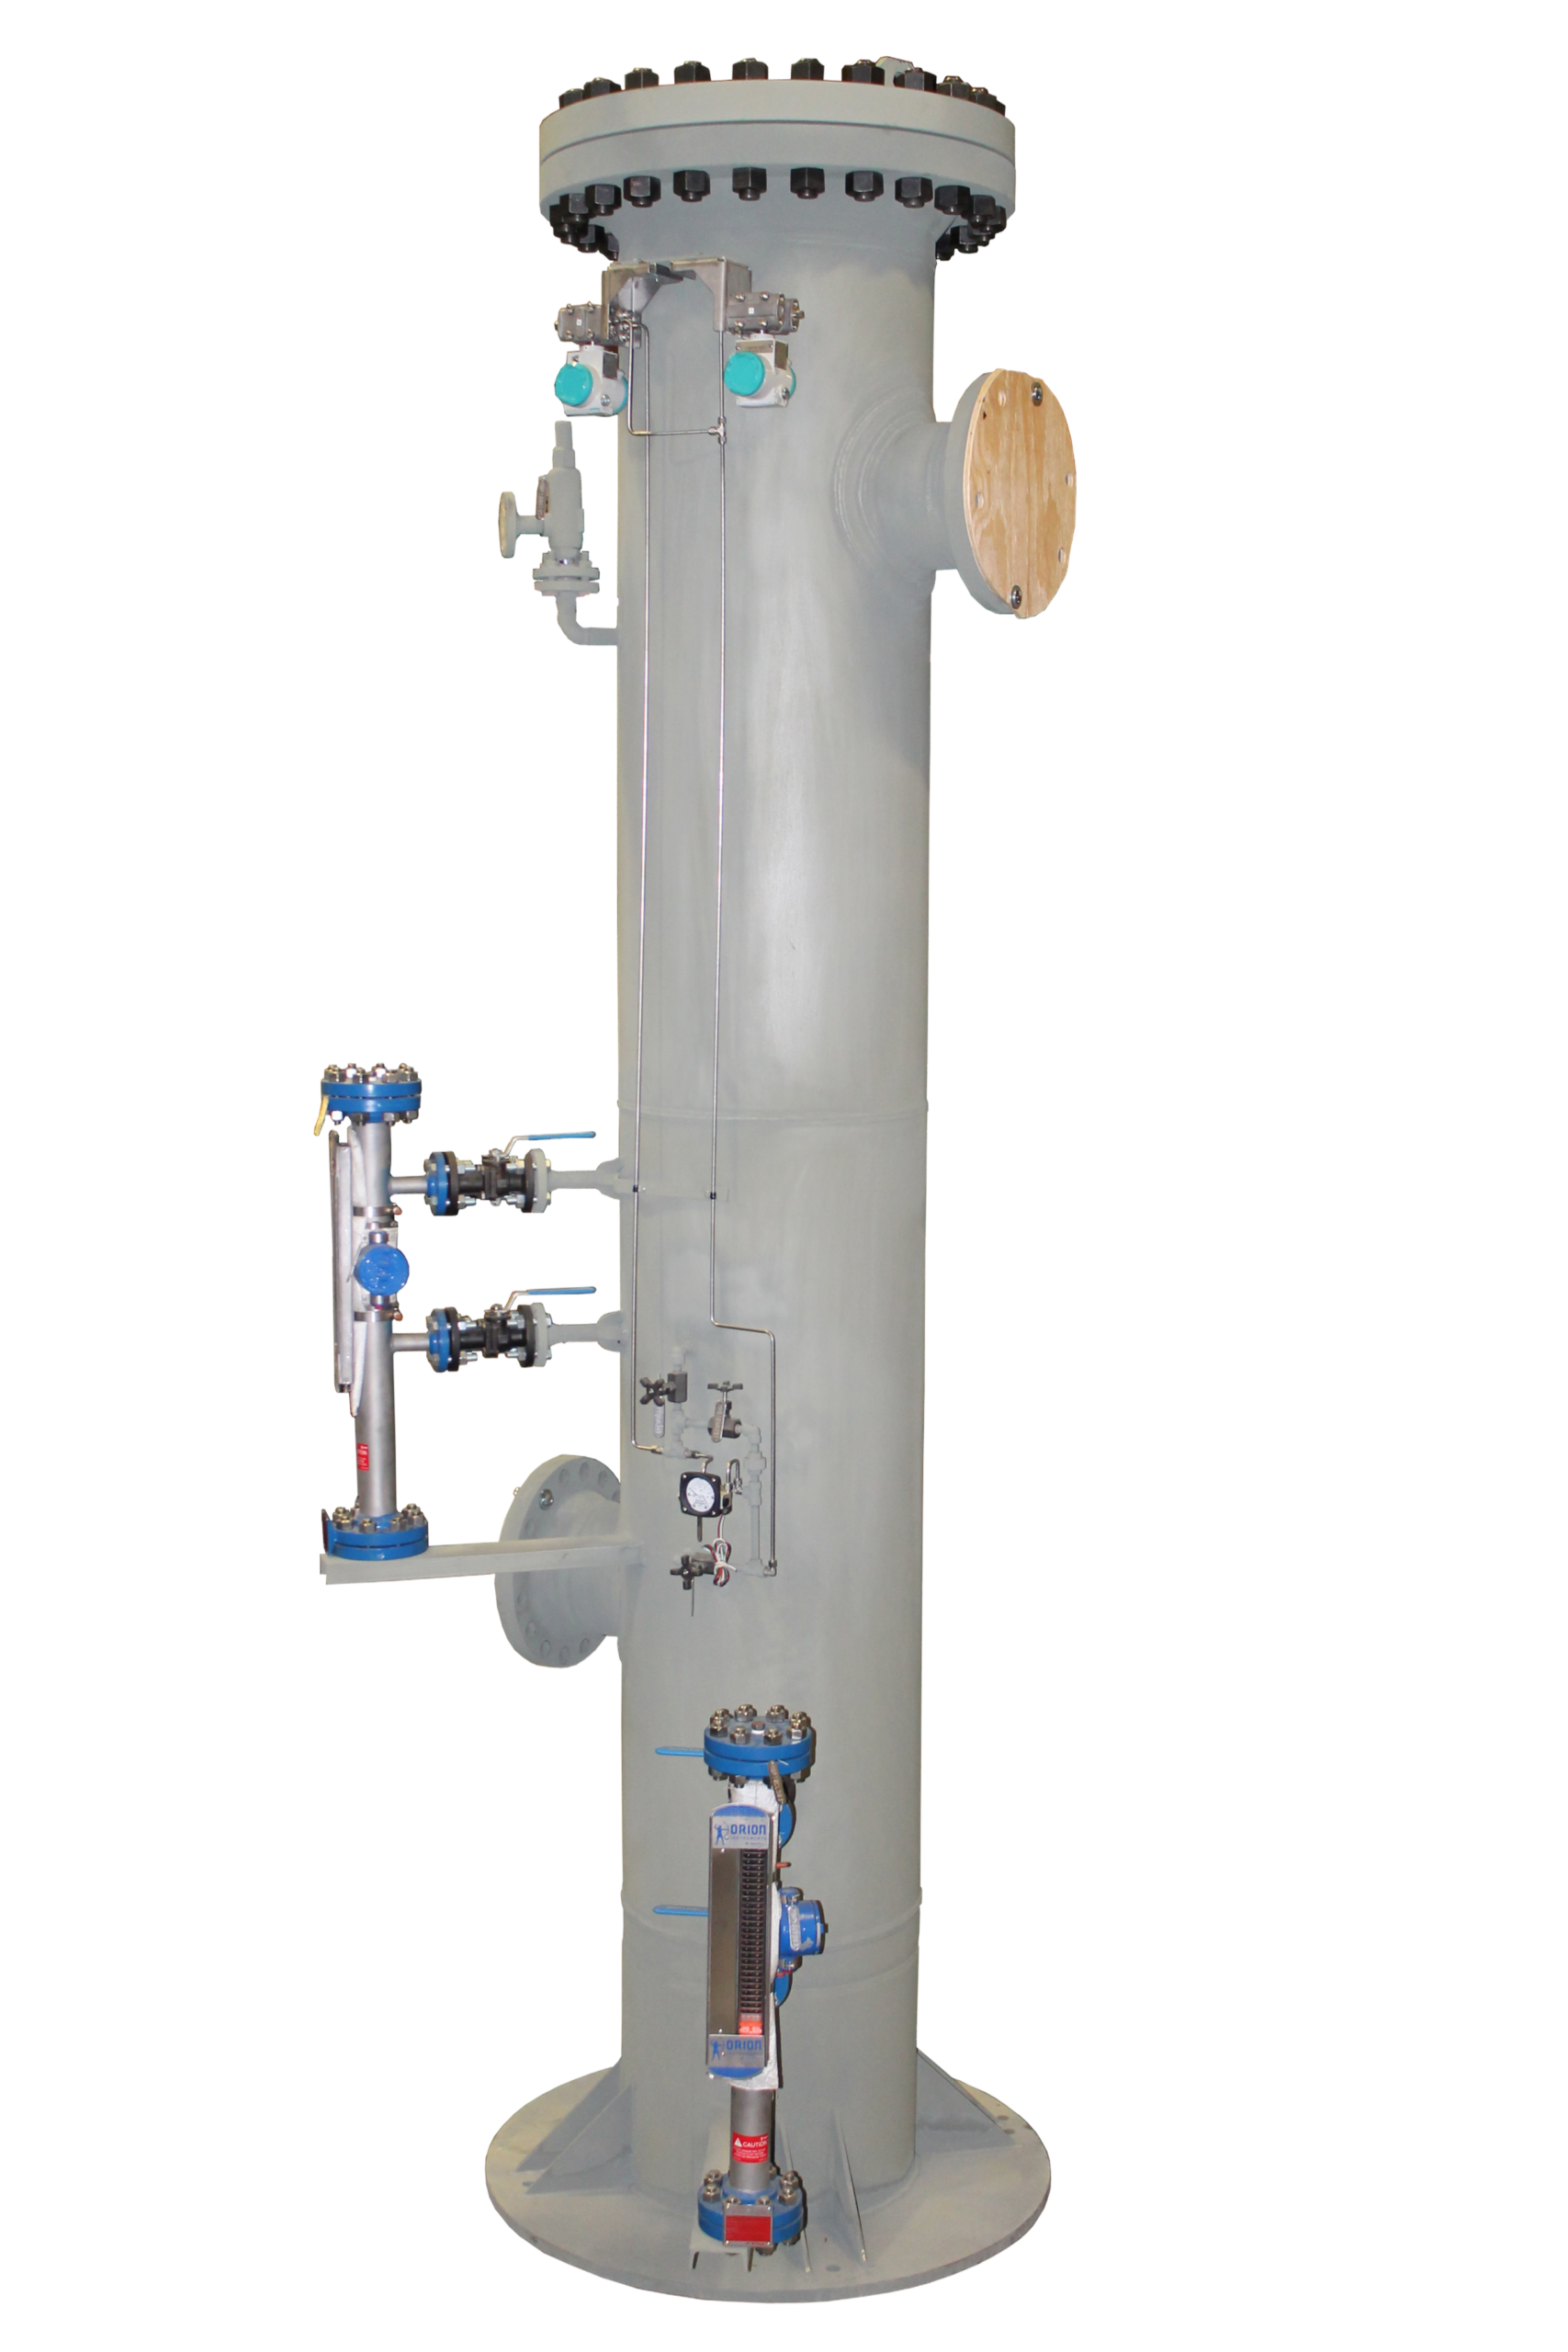
HILCO Gas Filter Separator Key Features:
Available in Simplex or Duplex Configurations
For uninterrupted engine operations HILCO Fuel Gas Vessels can be designed in simplex or Duplex configurations for continuous service during cartridge change outs. HILCO duplex filters come with HILCO ball valves tested to ANSI / FCI 70-2 class IV leakage requirements.
Heated Fuel Gas Applications
HILCO vessels can be designed to filter high temperature gases of up to and beyond 500°F (260°C).
Trusted by the OEM’s
Trusted by OEM’s world wide as “last chance” filters before fuel gas entered the turbine with the ability to filter down to 0.3 micron at 99.99% efficiency of solids.
Compatibility Across a Wide Range of Applications
Suitable for a wide range of different size turbines.
how it works
HILCO Filtration Equipment
Since HILCO’s founding in 1915, our filtration equipment has earned a trusted reputation among both Original Equipment Manufacturers (OEMs) and end users worldwide. This reputation is built on a long legacy of filtration expertise combined with world-class manufacturing capabilities.
One of HILCO’s defining advantages is our fully integrated design approach: every filtration system features a precisely engineered HILCO vessel paired with a perfectly matched HILCO cartridge, both manufactured at the same facility. This level of control ensures optimal performance, reliability, and consistency across all products.
By manufacturing both vessels and cartridges as a complete system, HILCO has not only established the industry benchmark for filtration performance but has continually raised the standard for more than a century.
Why Does Filtration Performance Matter?
Extended Equipment Life
Protects equipment by ensuring precision filtration across many different applications, fluids, and gases.
Longer Filter Element and Vessel Service Life
Ensures longer run time of key or critical components by providing extend filtration from the elements and long service life of the vessels.
Lower Maintenance Costs
Reduced risk of unplanned shutdowns in critical equipment
Custom Engineered and Standard Products
Wide range of standard products or custom engineered applications.
Industries
Fuel Gas Filters / Separators Trusted Across Critical Industries
HILCO Fuel Gas Filters / Separators Trusted by OEM’s and end users worldwide to ensure smooth continuous clean operation of flow into their turbines.
WHY HILLIARD
Why Companies Choose HILCO Equipment
Application-Focused Engineering
Over a century of filtration expertise, with custom and standard products engineered to OEM standards not just setting the bar but raising it.
Flexible Manufacturing Capabilities
In-house manufacturing gives Hilliard the flexibility to adapt standard products to new applications and respond quickly to customer needs.
Quality You Can Count On
ISO 9001:2015-certified, with strict quality standards backed by industry approvals, including ASME, PED, and API.
Support Beyond the Product
A global distributor network, technical support, and HILCO Lab Services keep your systems running long after the cartridges are installed.
Browse Categories
Products Supporting Critical Industrial Applications
Founded in 1905, Hilliard has grown from a one-product business into a global manufacturer serving customers across motion control
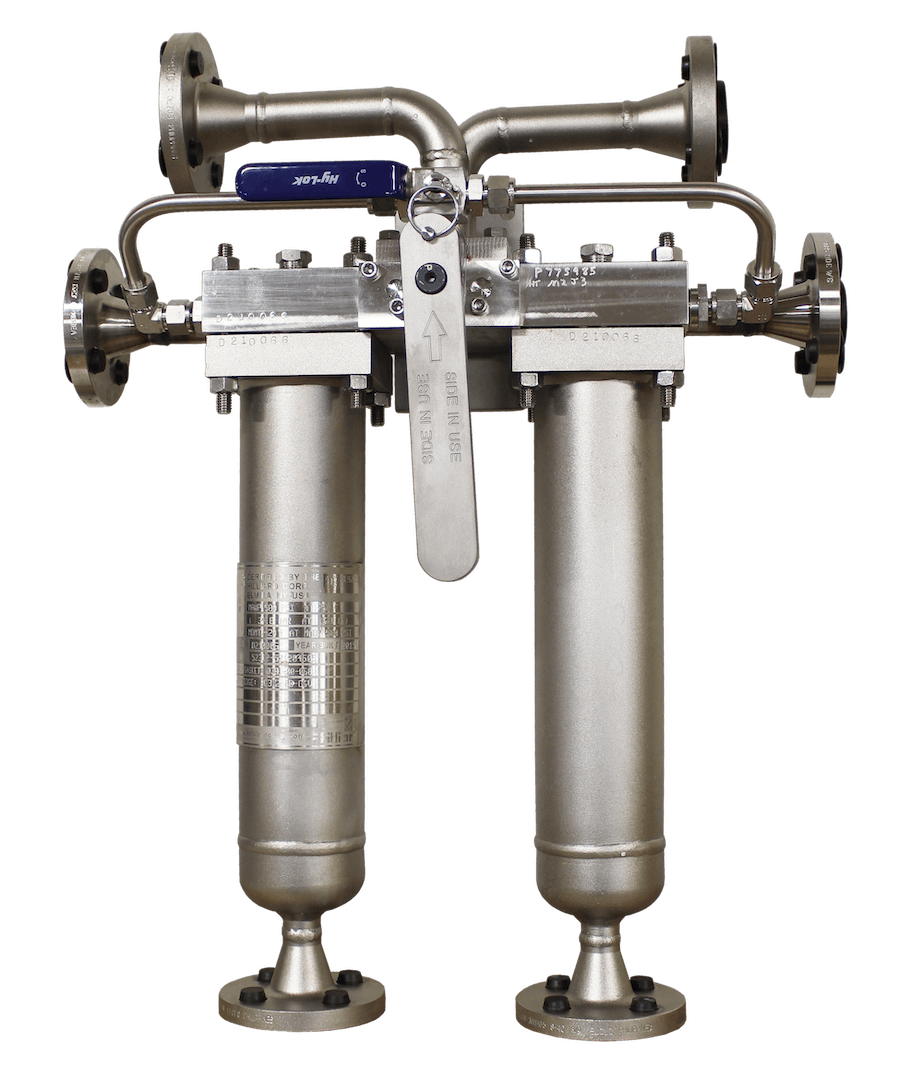
Filter Equipment
Complete filtration, separation, and fluid conditioning systems for industrial applications.
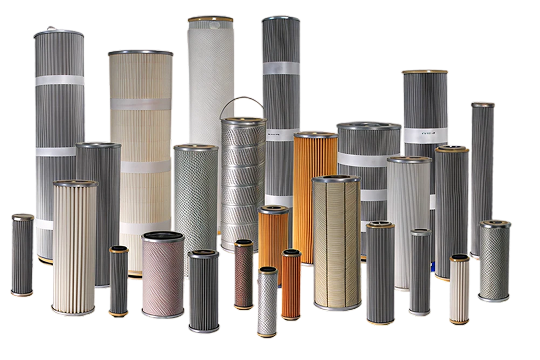
Filter Cartridges
High-performance filtration media for contamination control and fluid cleanliness.
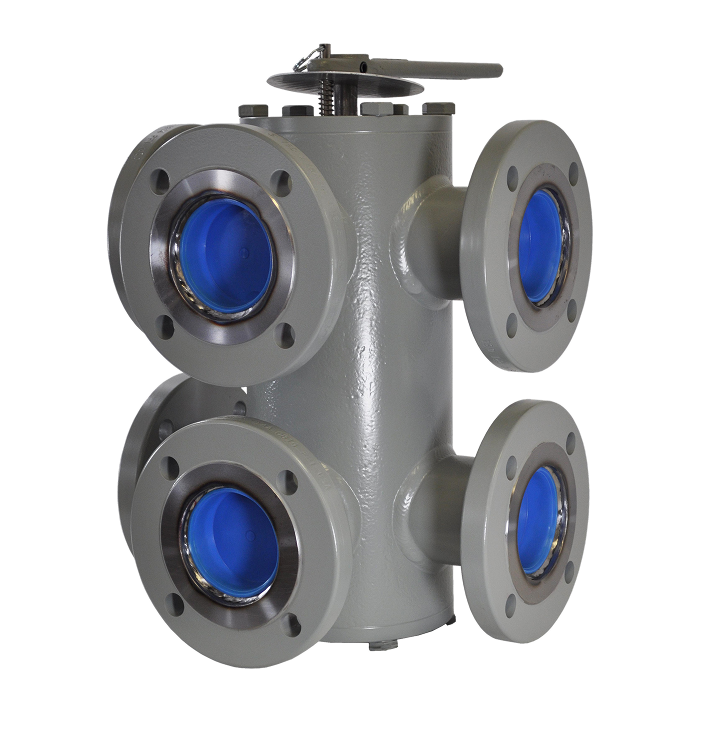
Valves
Industrial valve technologies for fluid isolation, flow diversion, and process control.
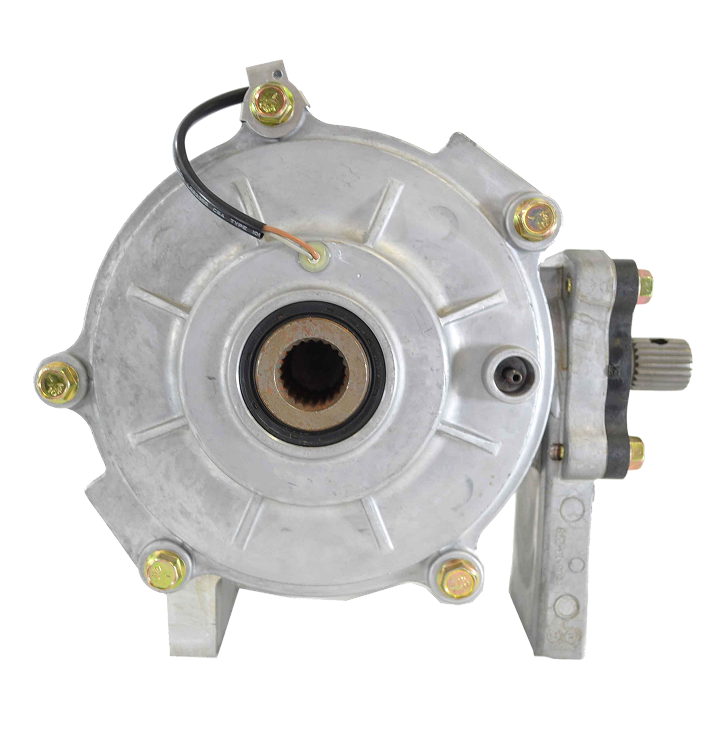
Drivetrain
Mechanical drivetrain systems for power transfer, traction control, and variable speed operation.
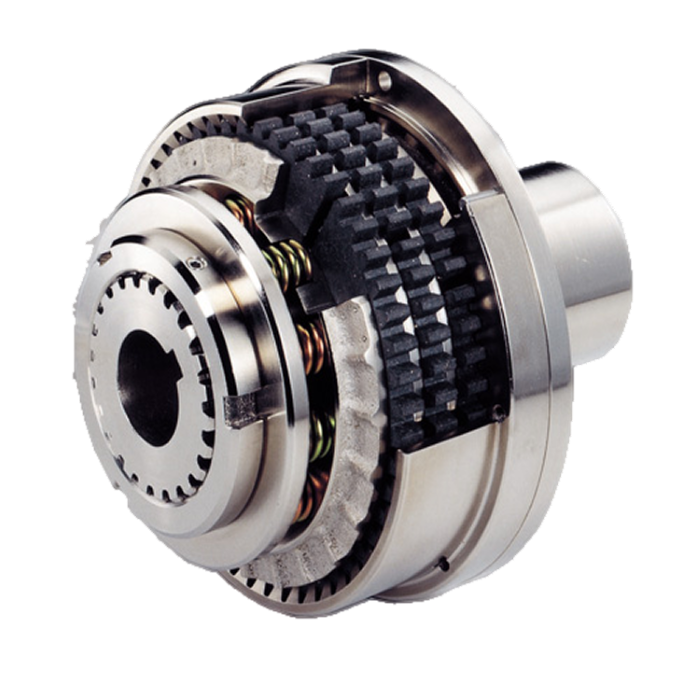
Motion Control
Clutch and torque limiting technologies for controlled power transmission and equipment protection.
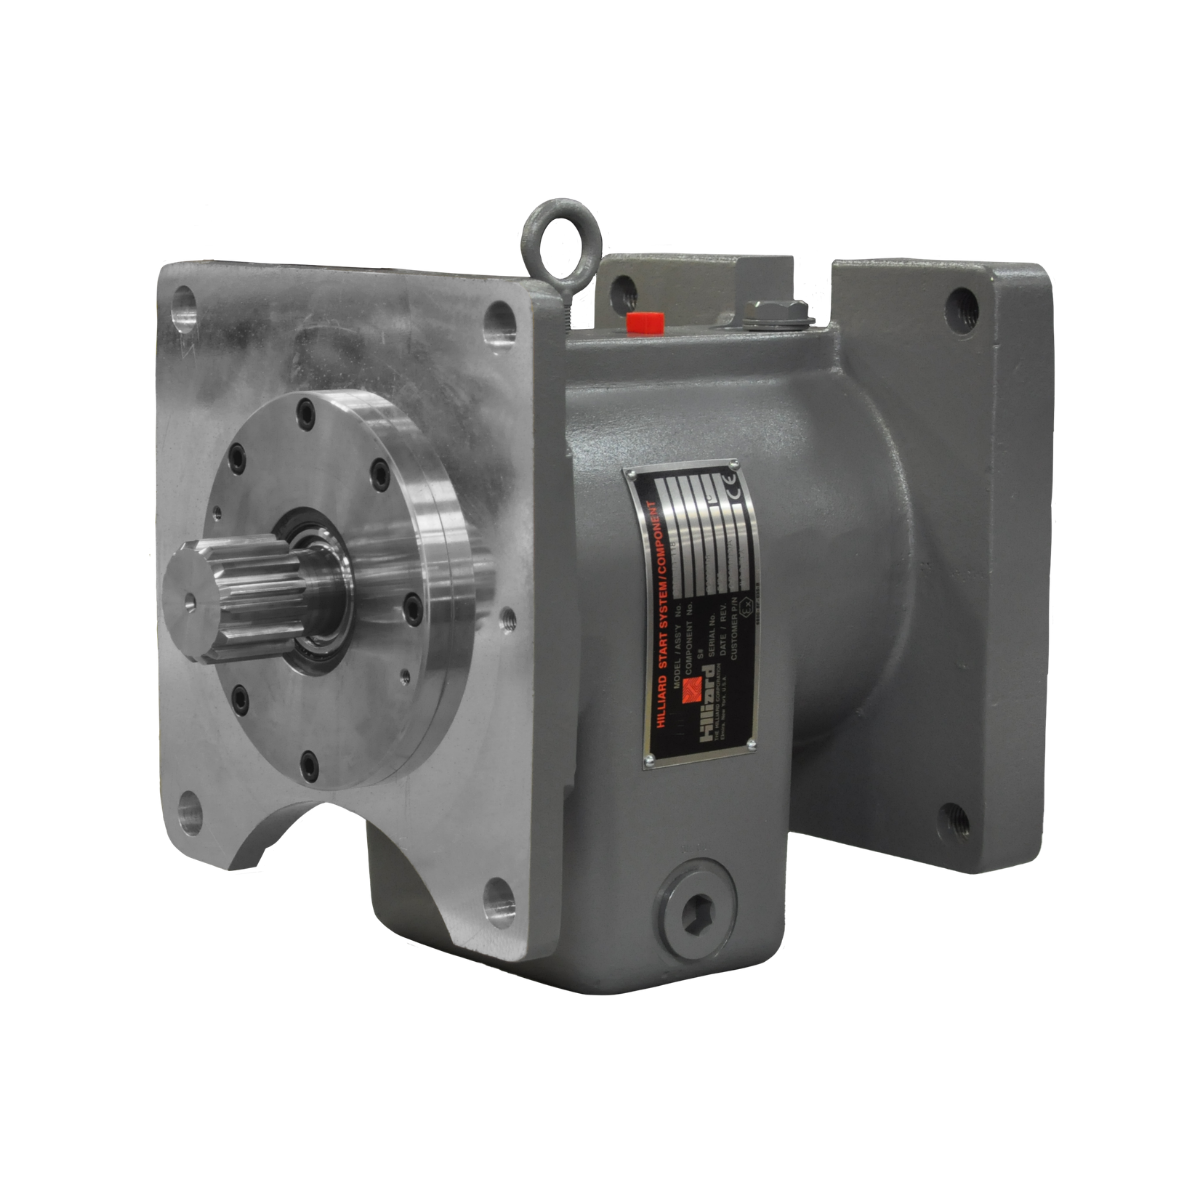
Engine Starters
Electric, hydraulic, and pneumatic starting systems for industrial engines and turbines.
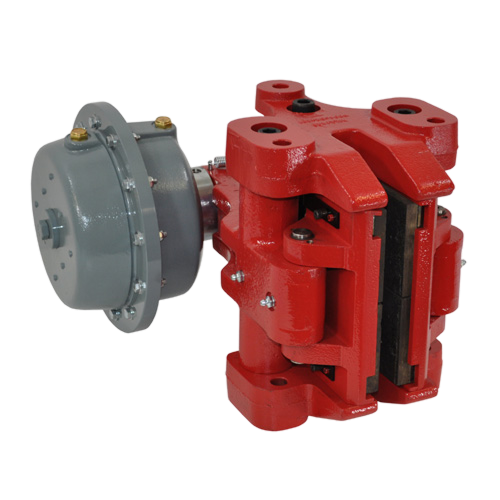
Industrial Braking Systems
Industrial braking technologies for stopping, holding, positioning, and controlled deceleration.
Engineered Filtration Equipment Built Around Your Application
Contamination Control
Fluid Management
Equipment Protection