Landfill
Supporting landfill gas collection, fluid handling, and environmental infrastructure through filtration, separation, and fluid management for demanding operating conditions.
Filtration and Separation Technologies for Landfill Operations
Landfill facilities rely on a combination of gas collection systems, fluid handling equipment, environmental infrastructure, and site operations to support daily activities. These systems must operate in environments where moisture, particulates, and contaminants are continuously present and can affect overall efficiency.
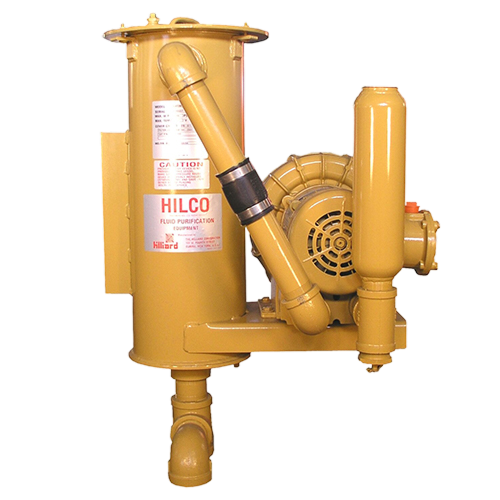
HILCO products are used in applications where filtration, separation, and fluid management play an important role in maintaining dependable operation across landfill facilities.
Browse Categories
Landfill Products
Founded in 1905, Hilliard has grown from a one-product business into a global manufacturer serving customers across motion control
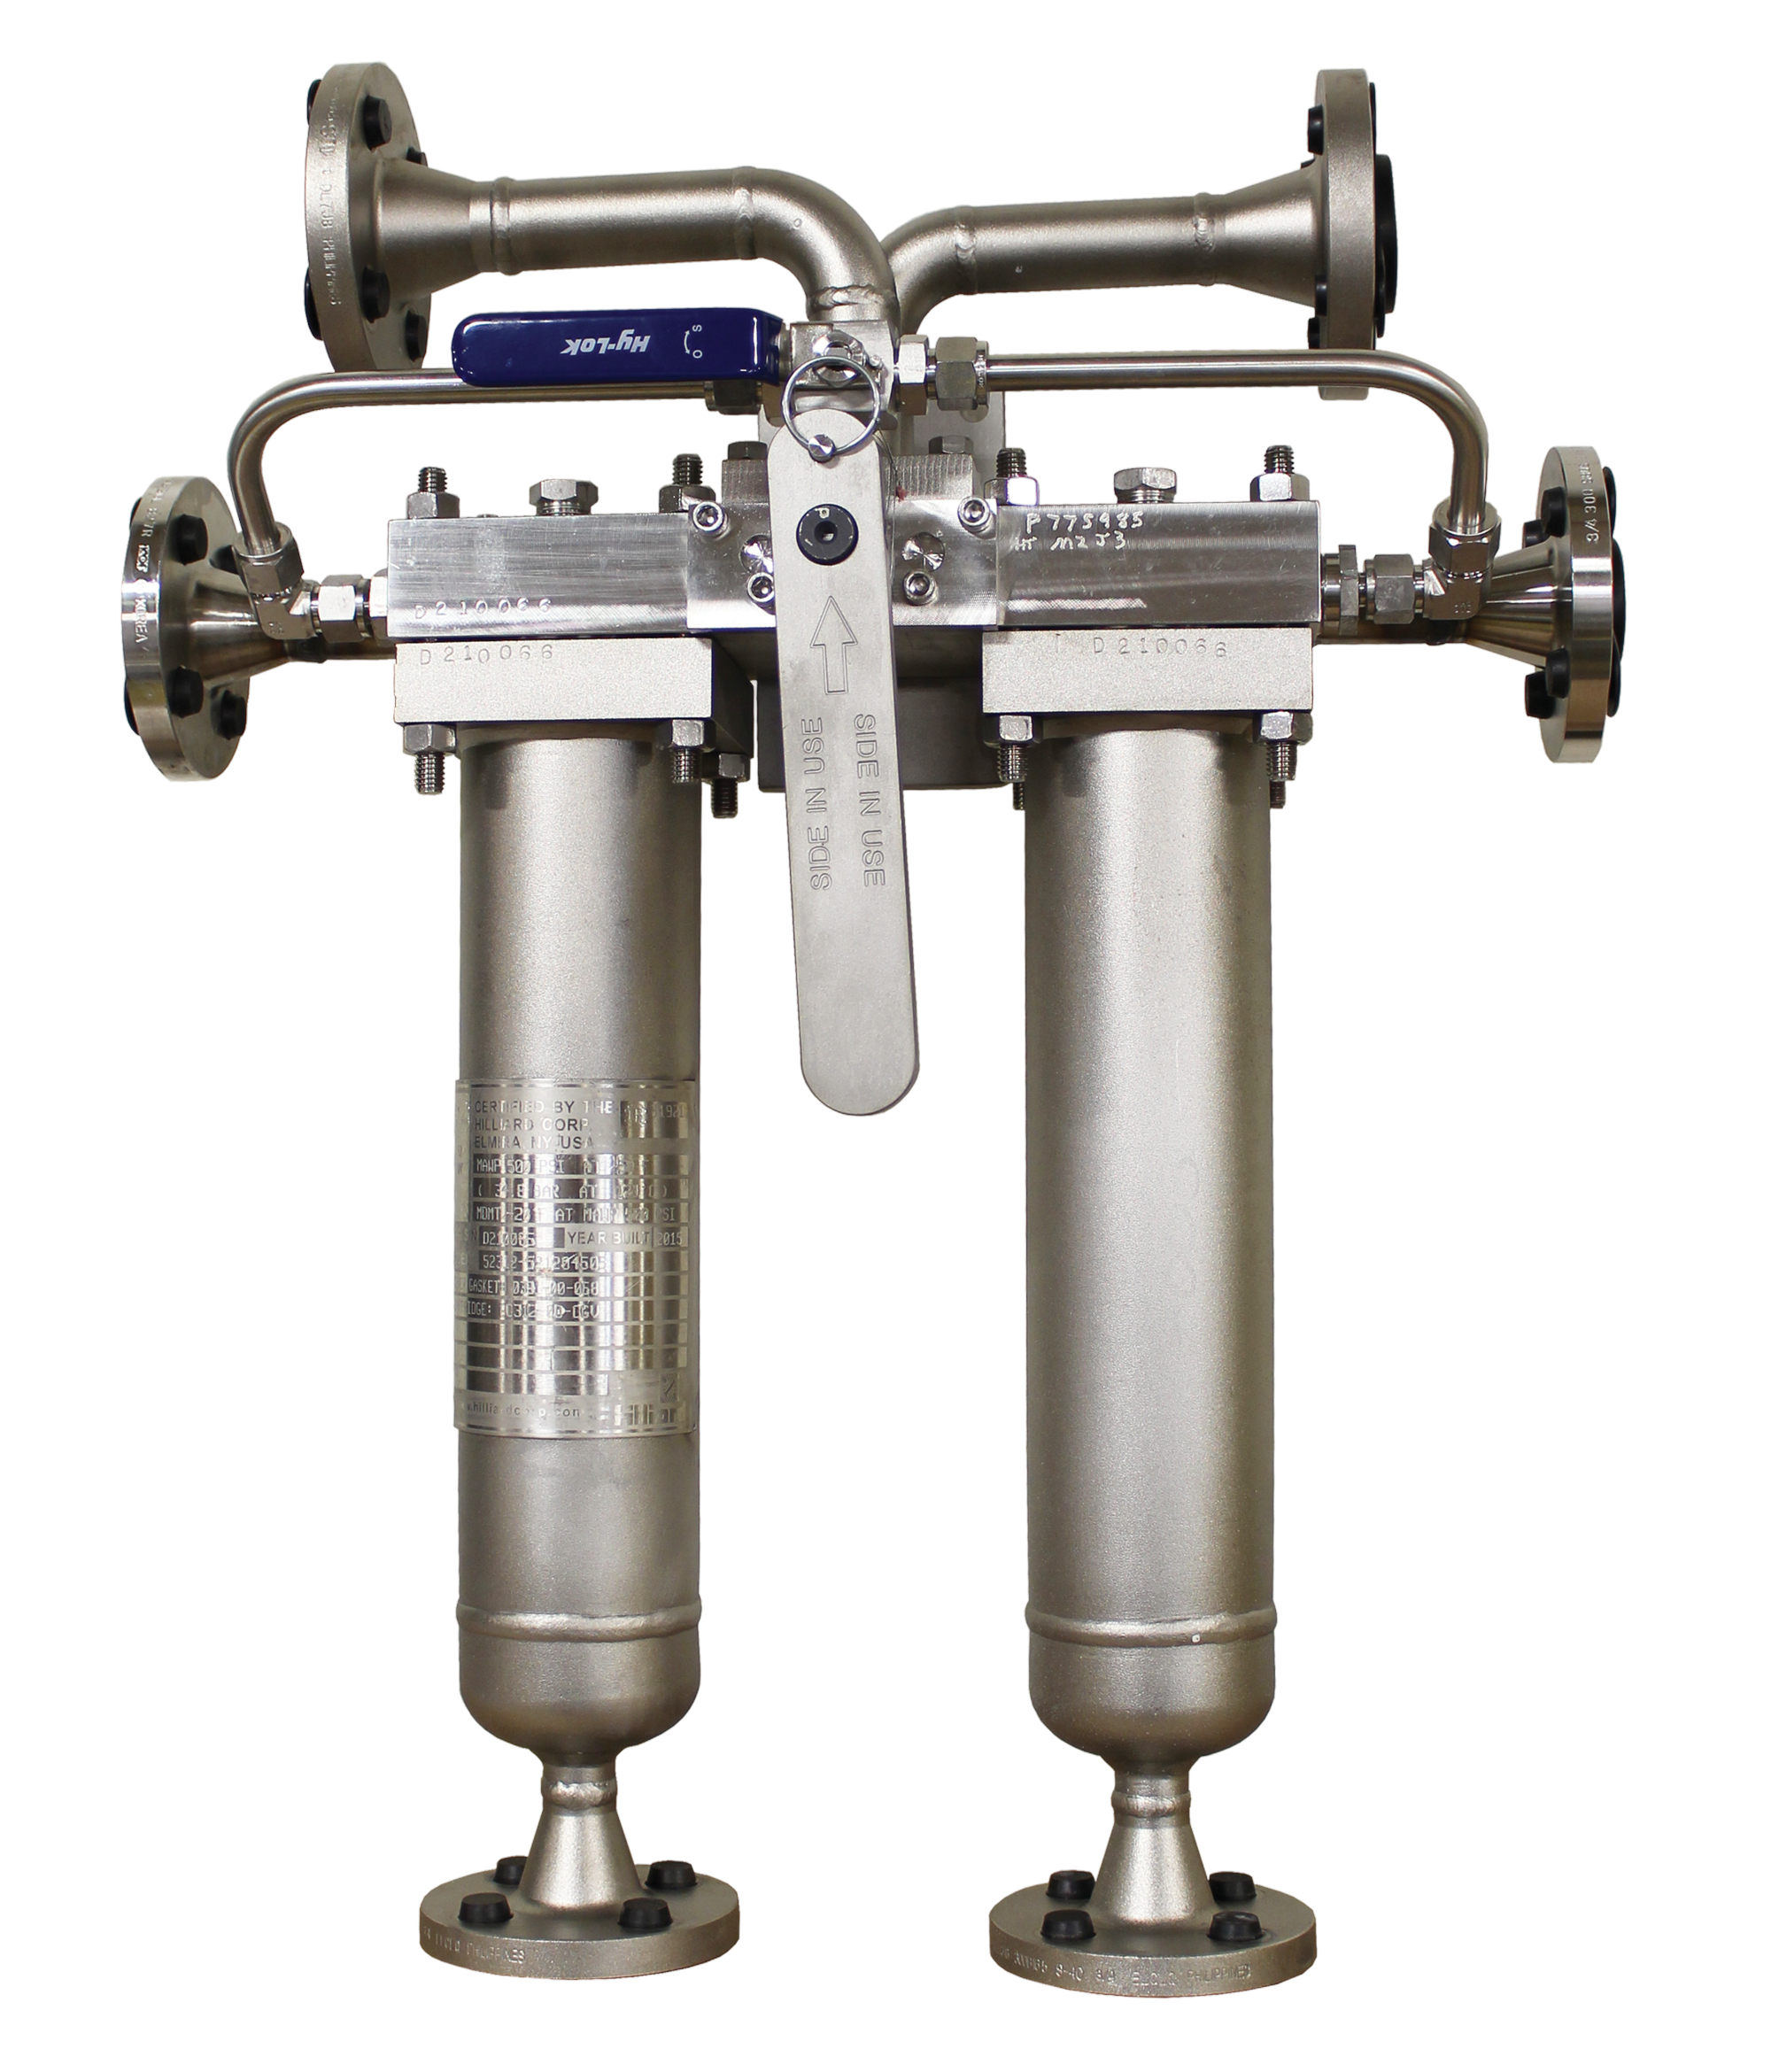
Filter Equipment
Complete filtration, separation, and fluid conditioning systems for industrial applications.
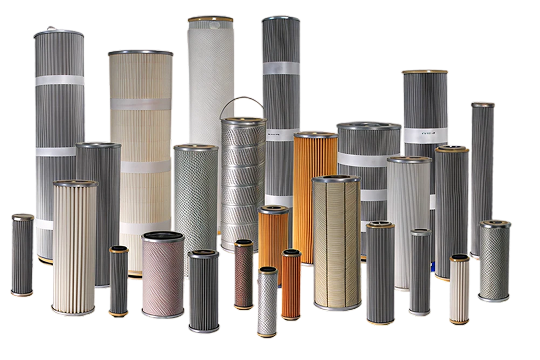
Filter Cartridges
High-performance filtration media for contamination control and fluid cleanliness.
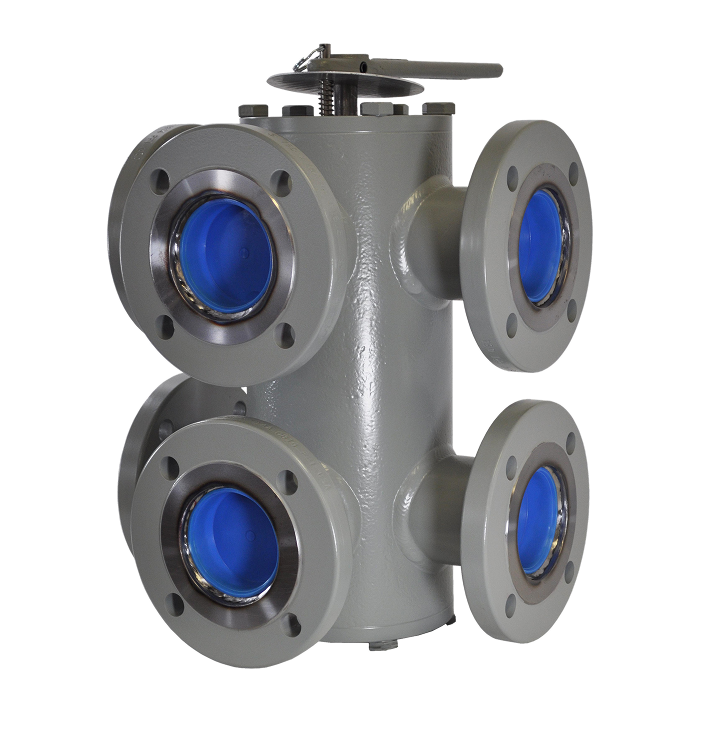
Valves
Industrial valve technologies for fluid isolation, flow diversion, and process control.
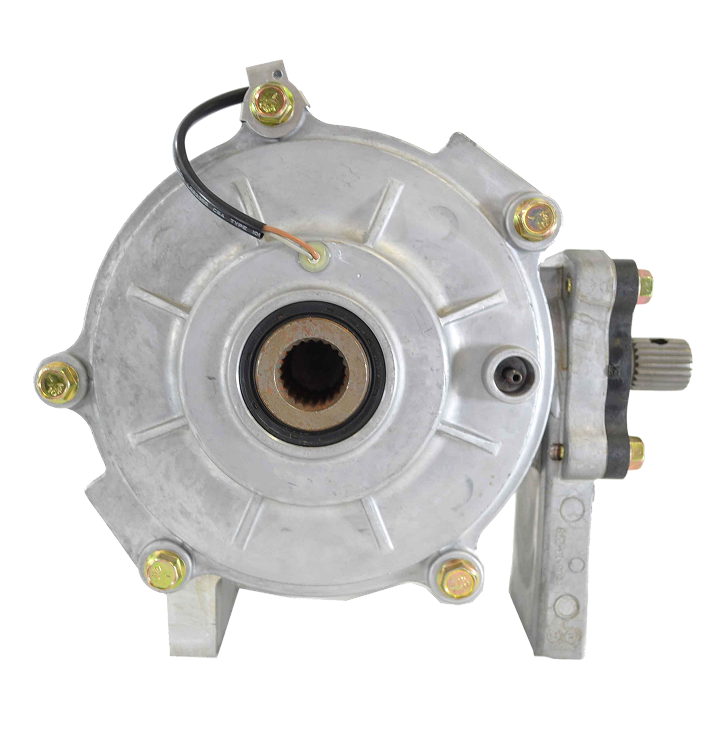
Drive Train
Mechanical drivetrain systems for power transfer, traction control, and variable speed operation.
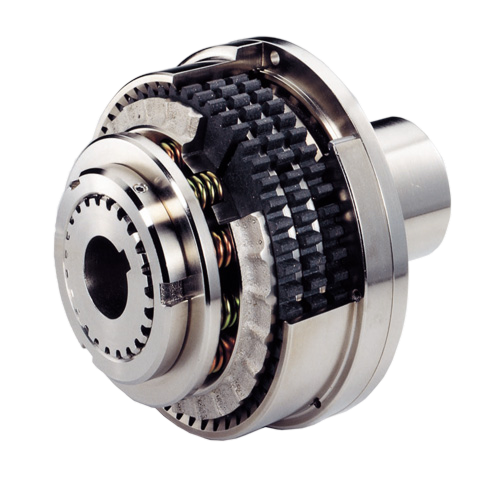
Motion Control
Clutch and torque limiting technologies for controlled power transmission and equipment protection.
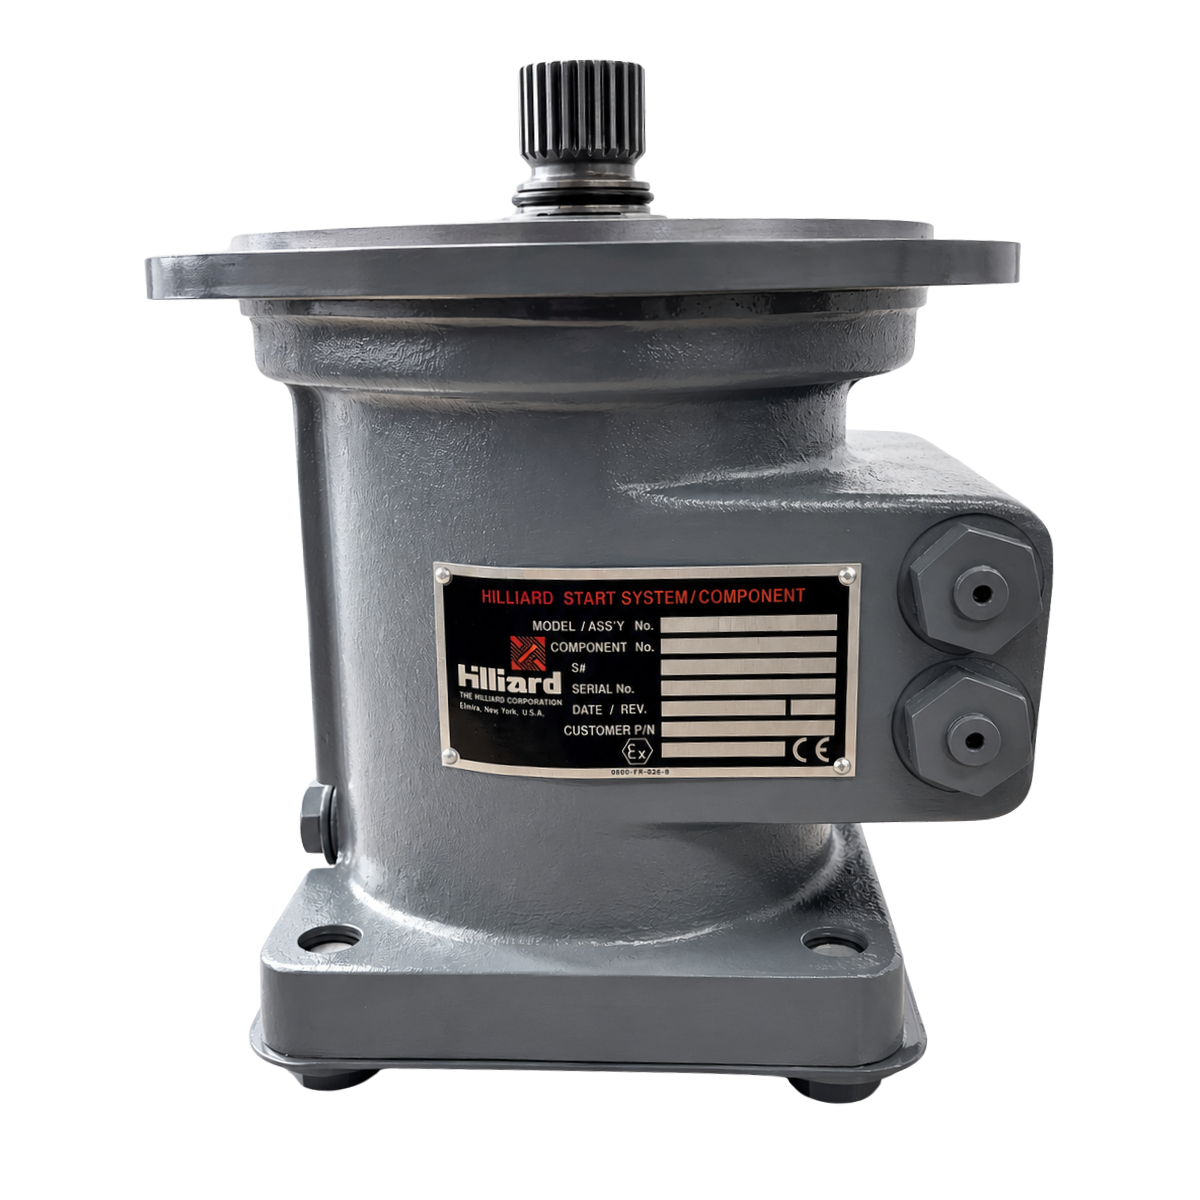
Engine Starters
Electric, hydraulic, and pneumatic starting systems for industrial engines and turbines.
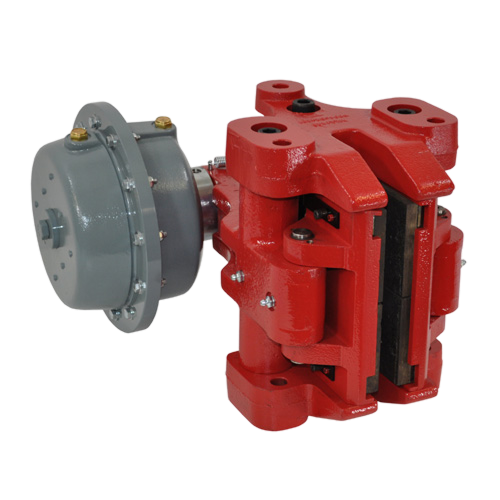
Industrial Braking Systems
Industrial braking technologies for stopping, holding, positioning, and controlled deceleration.
benefits
Managing Moisture, Particulates, and Contaminants
Landfill environments create conditions where contaminants can enter fluid and gas streams, affecting downstream processes and equipment. Effective filtration and separation help facilities maintain cleaner systems and address operational challenges associated with these demanding conditions.
HILCO Products for Landfill Applications
Particulate Removal
Filtration technologies help capture contaminants that can affect fluid and process systems.
Liquid Separation
Coalescing and separation products help remove unwanted liquids from gas streams and related applications.
Cleaner Operating Systems
Supports applications where contamination control is important to maintaining efficient operation.
Application Knowledge
Engineering expertise helps identify technologies appropriate for specific landfill requirements.
Featured Case Study or Use Case
Supporting Landfill Gas and Fluid Handling Systems
Landfill facilities utilize a variety of systems to manage gas collection, fluid movement, and supporting infrastructure throughout the site. Maintaining these systems often requires technologies capable of addressing moisture, particulate contamination, and changing operating conditions.
Condition Gas Streams
Remove liquids and contaminants before they reach downstream equipment.
Maintain Fluid Quality
Filter contaminants from operating fluids used throughout the facility.
Address Site-Specific Challenges
Apply filtration and separation technologies based on operating requirements.
Improve Process Consistency
Help maintain stable operation across critical landfill systems.
WHY HILLIARD
Why Landfill Operators Choose HILCO
Designed for Challenging Process Conditions
Products engineered for applications where moisture, particulates, and variable operating conditions require dependable filtration and separation performance.
Application Expertise Across Site Infrastructure
Experience supporting landfill gas collection, fluid handling equipment, and process systems throughout environmental operations.
Broad Process Equipment Portfolio
Filtration, coalescing, separation, laboratory services, and technical support available to address multiple contamination challenges across a facility.
Engineering Support for Long-Term Operation
Application guidance and technical expertise help facilities select equipment that aligns with process requirements and long-term operating objectives.
Application-Focused Products Backed by Engineering Expertise
Technical Knowledge
Proven Performance
Responsive Support