Industrial Oil Coalescer Separators
HILCO Lube Oil Coalescer Separators
Oil Coalescing Filter Separators for Industrial Applications
HILCO coalescer/separators are specifically designed to deliver reliable removal of moisture and particulate contamination from lubricating oils, helping maintain oil cleanliness, protect critical equipment, and extend service life.
Our coalescing filter separator systems provide dependable contamination control for power generation, refineries, petrochemical plants, steel mills, and other demanding industrial environments, helping reduce unplanned downtime and extend equipment life.
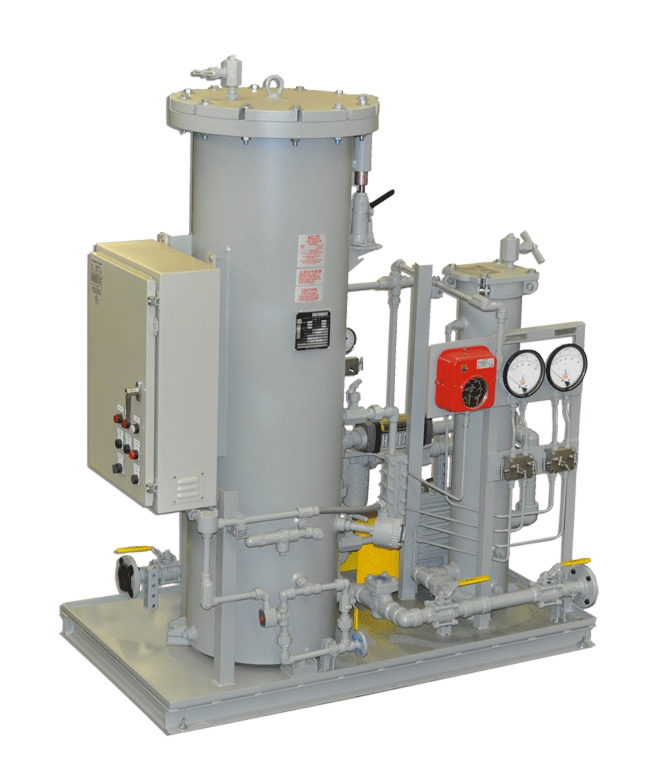
HILCO Coalescer Separators Key Features:
High-Efficiency Filtration and Water Removal
When combined with a HILCO coalescer/separator cartridge, systems achieve 99.5% particle removal efficiency at 3 microns. They can also remove and reduce free and emulsified water content to below 25 ppm and maintain total water content to below 150 ppm, based on a process stream containing 5% water.
Multiple Sizes and Flow Capacities
Available in standard sizes with flow rates from 10 to 100 GPM with the ability to service reservoir capacities up to 20,000 gallons.
Flexible Configurations
Customizable vessel connections, piping sizes, and controls to meet application requirements. Available with NEMA or IEC electrical enclosures and with or without a separator.
Domestic and International Code Compatibility
Available in ASME and non-ASME configurations, with applicable certifications and markings including UL, CSA, CE, ATEX, GOST, KESCO, NR-13, CRN, and PED.
FILTRATION EXPERTISE
HILCO’s Engineered Coalescing Filtration Systems for Lube Oil Water Removal
Since 1915, HILCO has provided industrial filtration solutions trusted by Original Equipment Manufacturers (OEMs) and end users worldwide. Backed by more than a century of filtration expertise and in-house manufacturing capabilities, HILCO develops standard and custom-engineered coalescer separator systems for demanding industrial applications.
HILCO coalescer separators combine particulate filtration and water separation to help maintain clean, dry lubricating oil. Specialized coalescing cartridges capture fine water droplets and combine them into larger droplets, allowing water to separate from the oil for removal.
Benefits of Effective Lube Oil Filtration and Water Separation
HILCO oil coalescer systems help maintain lubricant quality and deliver several operational benefits:
Extended Equipment Life
Helps protect critical equipment and lubricated components from wear and damage associated with moisture and particulate contamination.
Longer Filter Element and Vessel Service Life
Ensures longer run time of key or critical components by providing extended filtration from the elements and long service life of the vessels.
Lower Maintenance Costs and Reduced Downtime
Helps minimize contamination-related wear, and reduce the risk of unplanned equipment shutdowns.
Custom Engineered and Standard Products
Wide range of standard products or custom engineered applications to accommodate different flow rates, reservoir capacities, and operating requirements.
Industries
Industrial Coalescer Separator Systems Trusted Across Critical Applications
HILCO coalescer separator vessels support effective moisture and contamination control in lubricating oil systems across demanding environments, including:
WHY HILLIARD
Why Companies Choose HILCO Equipment
Application-Focused Engineering
HILCO engineers standard and custom coalescer separator systems around specific moisture removal, flow rate, and operating requirements.
Flexible Manufacturing Capabilities
HILCO manufactures engineered vessels and matched filtration cartridges in-house, supporting consistent filtration performance, quality, and reliability.
Quality You Can Count On
ISO 9001:2015-certified, with strict quality standards backed by industry approvals, including ASME, PED, and API.
Support Beyond the Product
HILCO provides technical support, replacement cartridges, and lab services to help maintain oil cleanliness and long-term filtration performance.
Browse Categories
Products Supporting Critical Industrial Applications
Beyond oil coalescer separators, HILCO offers a broad range of filtration equipment, cartridges, and fluid conditioning solutions designed to remove contaminants, maintain fluid cleanliness, and protect critical industrial equipment.
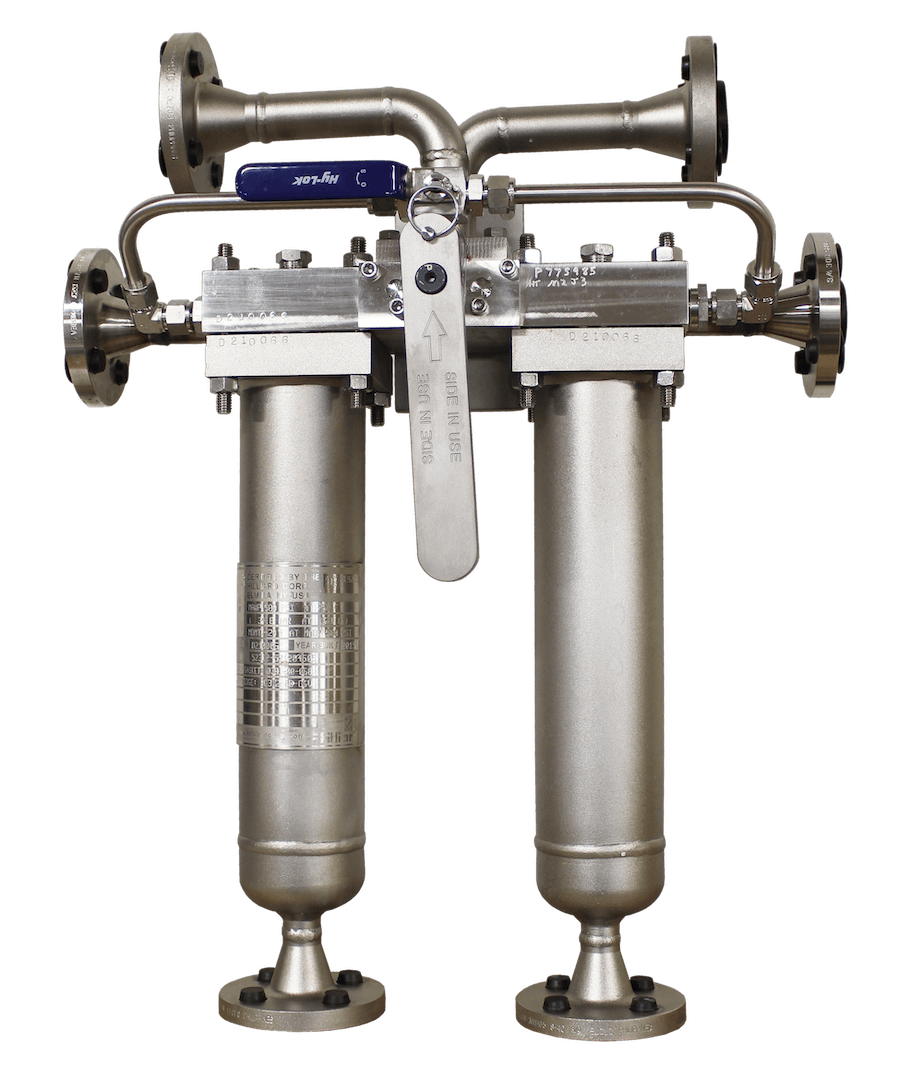
Filter Equipment
Complete filtration, separation, and fluid conditioning systems for industrial applications.
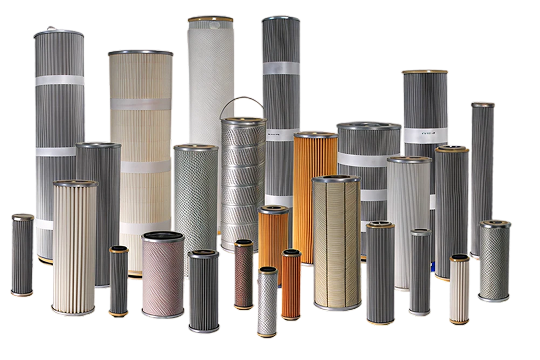
Filter Cartridges
High-performance filtration media for contamination control and fluid cleanliness.
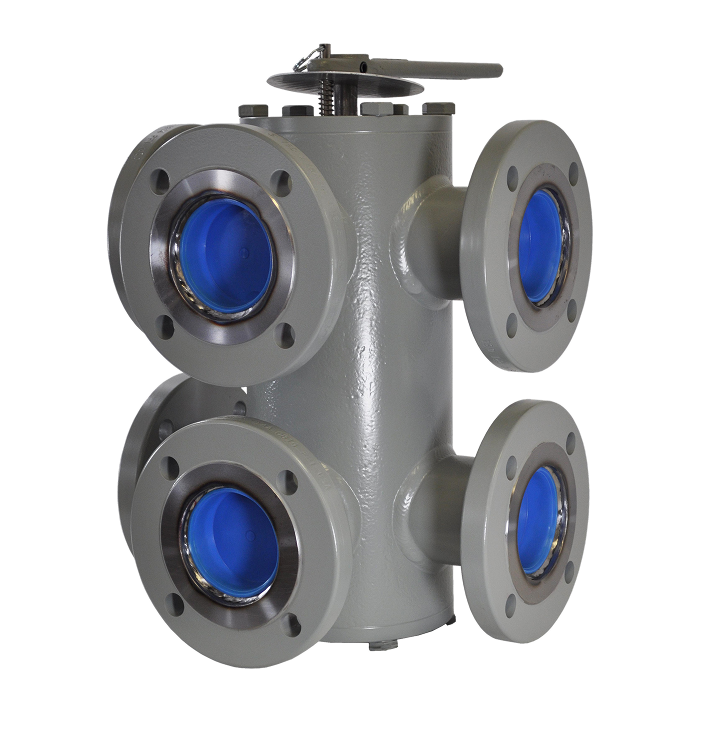
Valves
Industrial valve technologies for fluid isolation, flow diversion, and process control.
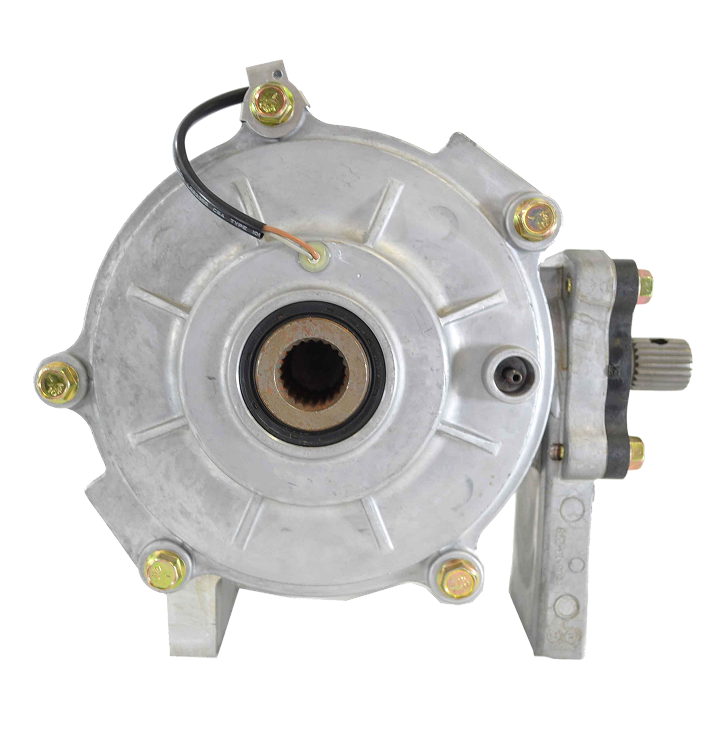
Drivetrain
Mechanical drivetrain systems for power transfer, traction control, and variable speed operation.
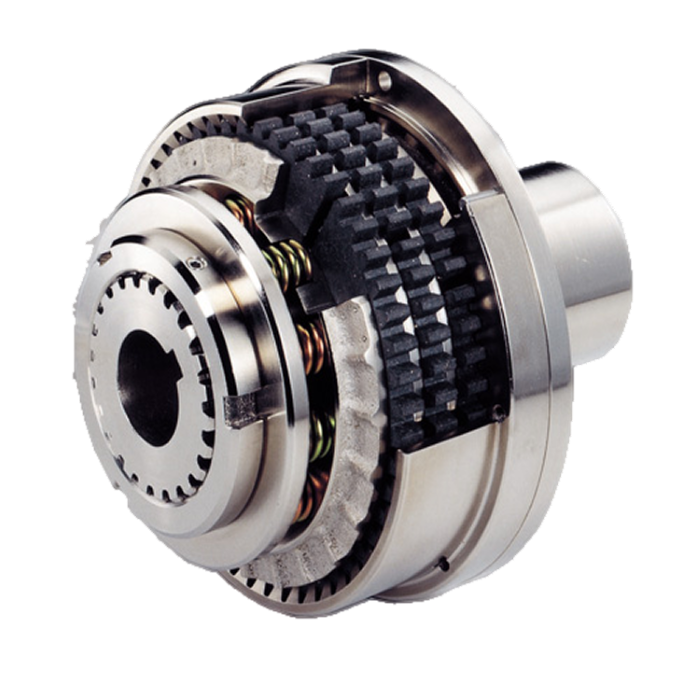
Motion Control
Clutch and torque limiting technologies for controlled power transmission and equipment protection.
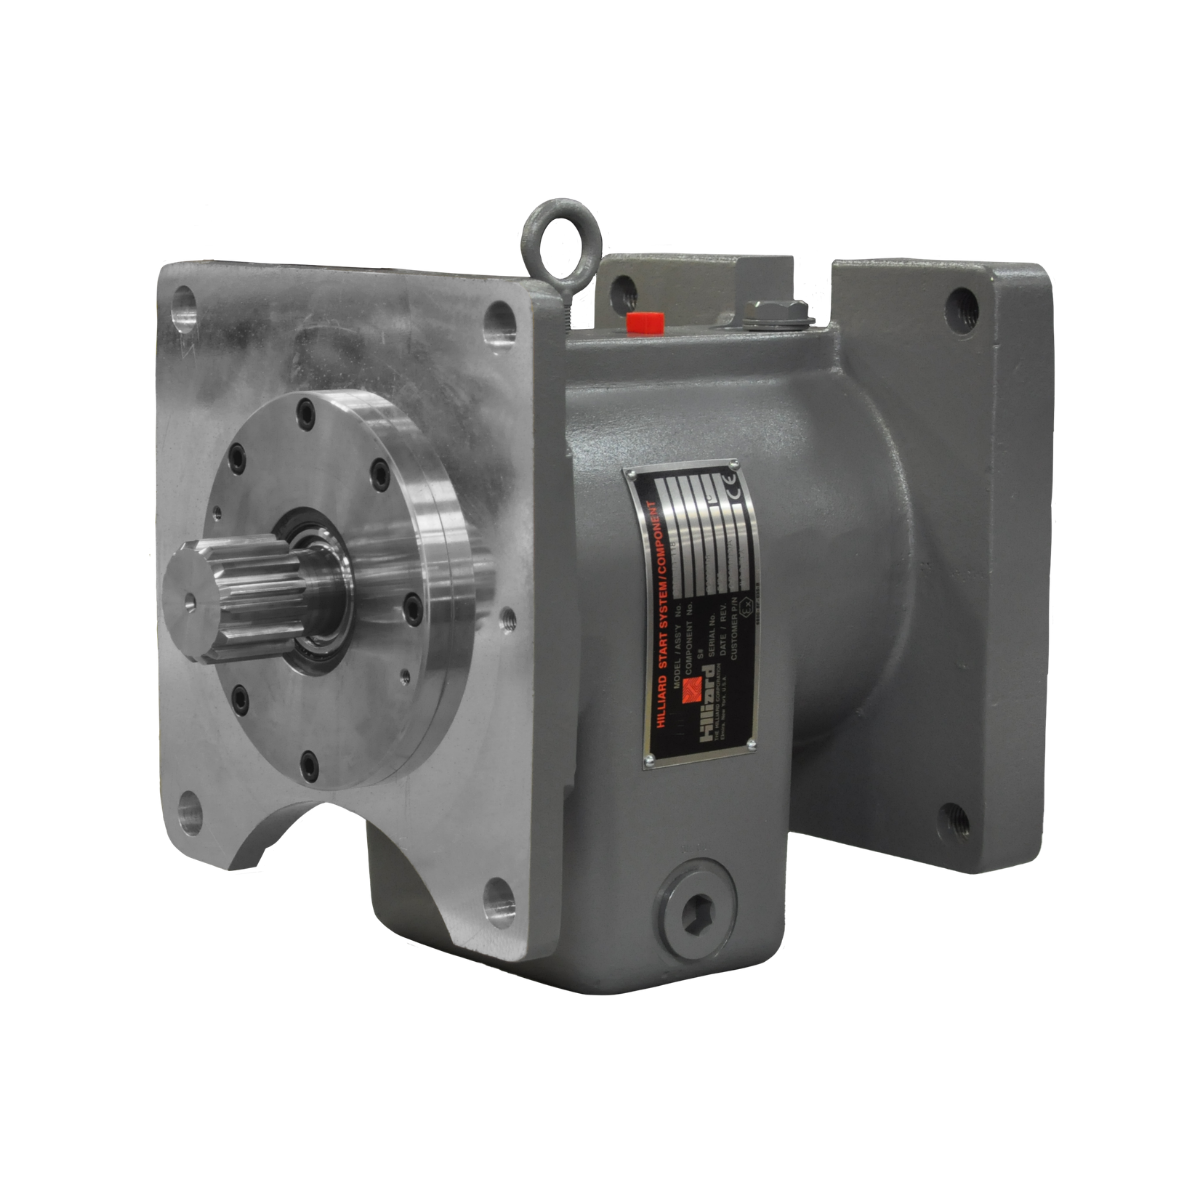
Engine Starters
Electric, hydraulic, and pneumatic starting systems for industrial engines and turbines.
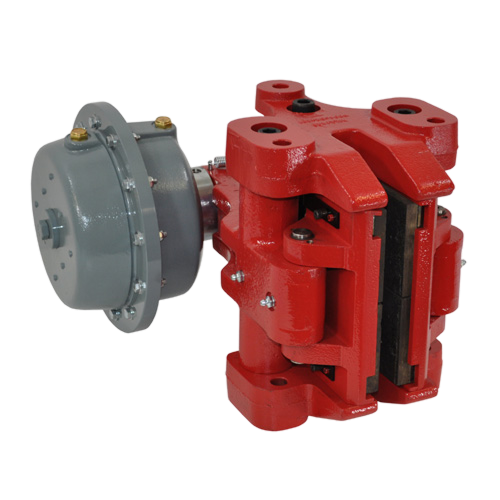
Industrial Braking Systems
Industrial braking technologies for stopping, holding, positioning, and controlled deceleration.
Engineered Oil Coalescer Separators Built Around Your Application
Contamination Control
Fluid Management
Equipment Protection