Industrial HiLite Filter Cartridges
HILCO HT Series
Fuller’s Earth Treatment for Fluid Stabilization
HILCO HT Series HiLite® Cartridges utilize a high-grade calcined fuller’s earth media to remove acids, oxidation byproducts, gum, and other polar contaminants from industrial fluids. Through a combination of adsorption and neutralization, HT Series cartridges help restore fluid condition, improve stability, and extend usable fluid life.
Hilite cartridges are commonly used in petroleum-based oils, transformer oils, turbine lubricants, heat transfer fluids, and other applications where fluid degradation products can impact performance and reliability.
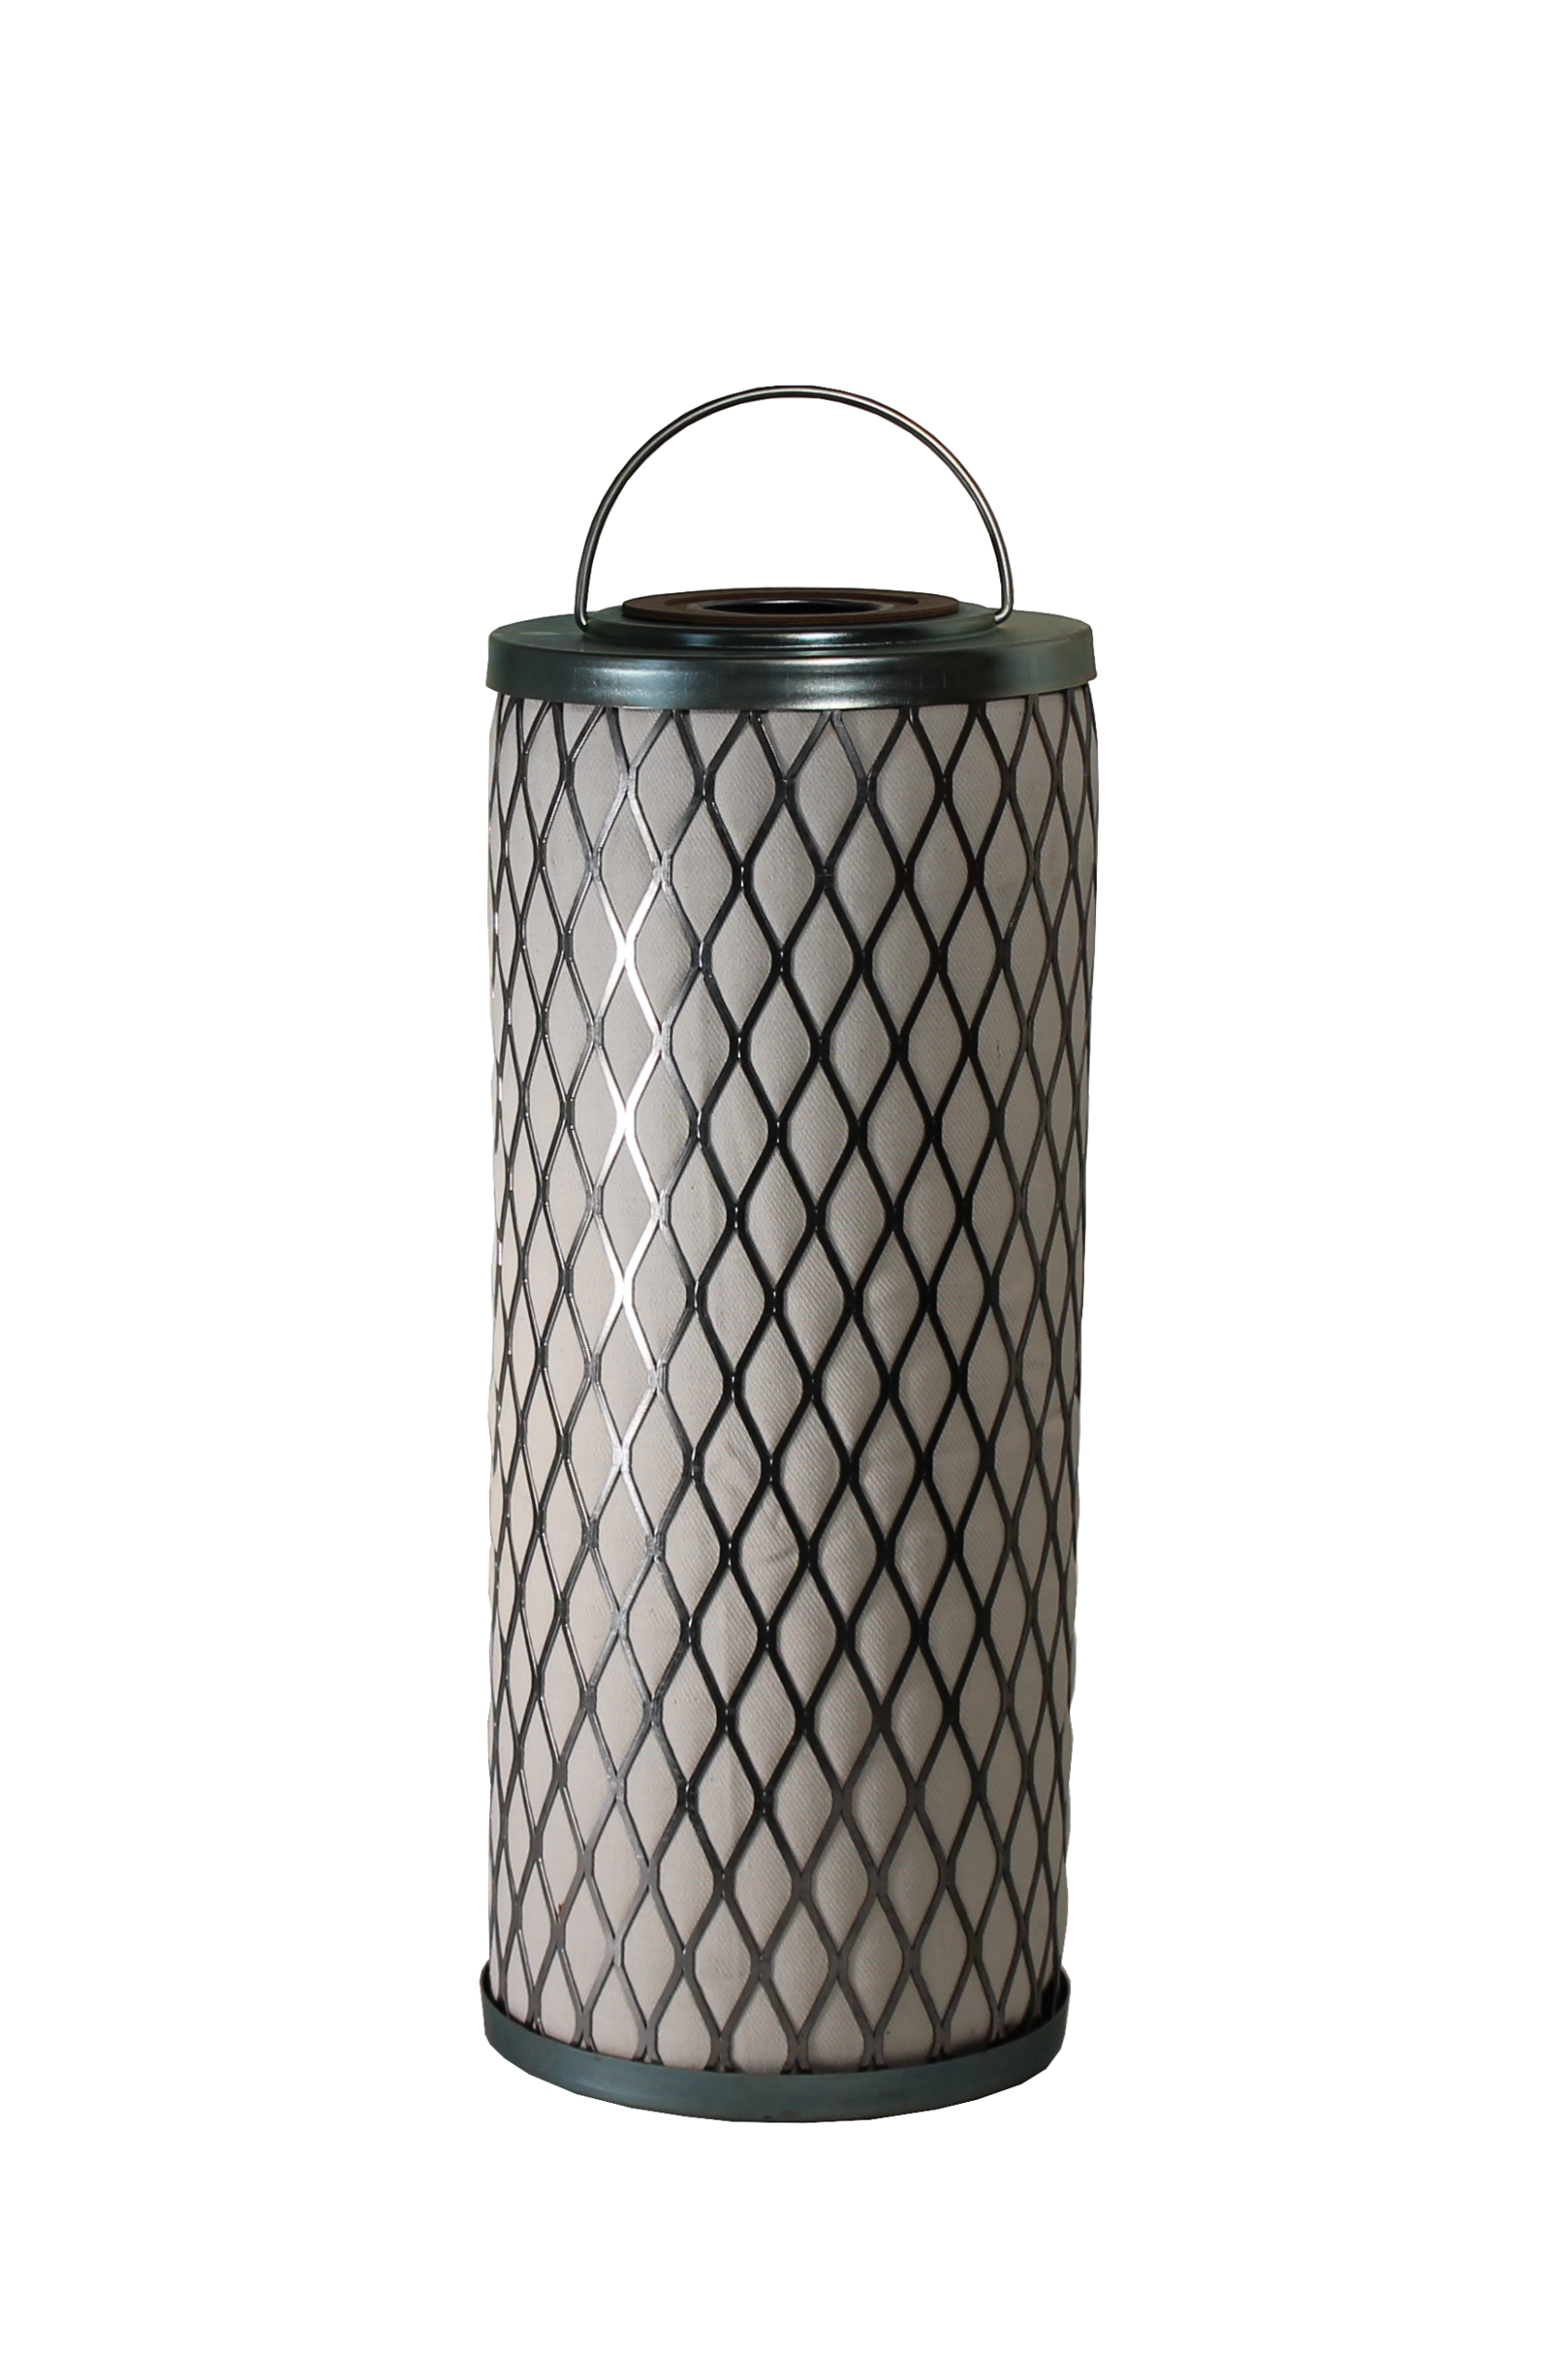
HILCO HiLite Cartridge Key Features:
Calcined Fuller’s Earth Media
Utilizes low-moisture-content attapulgite clay with high adsorption capacity for polar contaminants.
Acid Reduction Capability
Helps neutralize acidic degradation products that contribute to fluid deterioration and increasing TAN levels.
Adsorption of Oxidation Byproducts
Removes gums, resins, asphaltines, and other oxidation products that accumulate during fluid aging.
Fluid Color and Condition Restoration
Helps improve fluid appearance and maintain desirable operating characteristics.
Water-Resistant Media Construction
Calcined media provides greater resistance to moisture than conventional fuller’s earth products.
HOW IT WORKS
Adsorbing Acids and Oxidation Byproducts from Industrial Fluids
As industrial oils age, heat, oxidation, and chemical reactions gradually produce acidic compounds and other polar contaminants. These degradation products remain dissolved in the fluid, where they contribute to rising Total Acid Number (TAN), fluid instability, discoloration, and accelerated oxidation.
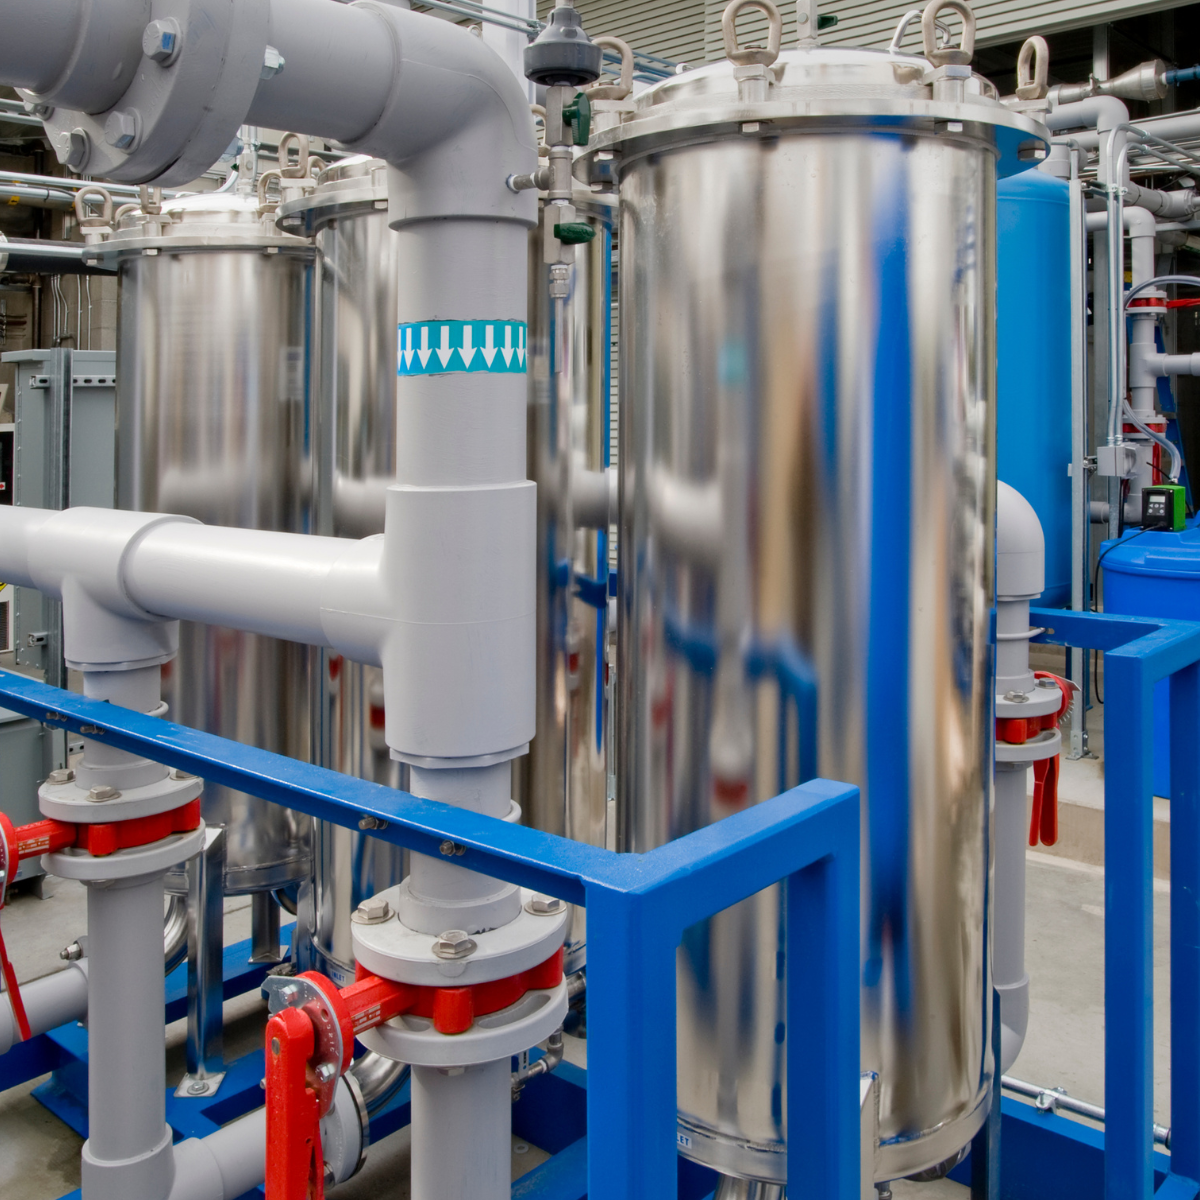
By removing degradation products from the fluid stream, HILCO HT Series HiLite Cartridges help deliver:
Acid Neutralization
Reduces acidic compounds that contribute to fluid degradation and increasing TAN levels
Adsorption of Polar Contaminants
Captures oxidation byproducts such as gums, resins, and asphaltines before they continue circulating through the system
Fluid Stabilization
Slows the progression of oxidation by removing compounds that promote further degradation
Color and Clarity Improvement
Helps restore fluid appearance by removing contaminants responsible for discoloration
HT Series cartridges contain highly porous calcined fuller’s earth media with an exceptionally large internal surface area. As fluid passes through the acid removal cartridge, acidic compounds and other polar contaminants are attracted to and retained within the media structure. The treated fluid exits with reduced concentrations of degradation byproducts, helping maintain fluid condition and extend service life.
Industries
Fluid Reclamation Across Critical Industrial Applications
HILCO HT Series HiLite Cartridges are used in applications where oxidation byproducts, acid formation, and fluid degradation must be controlled to maintain fluid quality and equipment reliability.
WHY HILLIARD
Why Companies Choose HILCO HiLITE Filter Cartridges
High-Efficiency Synthetic Filtration
HiLITE cartridges use synthetic filtration media designed for efficient particulate removal in demanding industrial lubrication and hydraulic systems.
High Dirt-Holding Capacity
The cartridge construction provides substantial contaminant-holding capacity, supporting effective filtration throughout the element’s operating life.
Consistent Particle Removal Performance
HiLITE media provides controlled filtration performance to maintain fluid cleanliness and protect contamination-sensitive system components.
Engineered for HILCO Filtration Systems
HiLITE cartridges combine HILCO filtration media technology with application engineering and equipment expertise for integrated industrial contamination control.
Browse Categories
Products Supporting Critical Industrial Applications
Founded in 1905, Hilliard has grown from a one-product business into a global manufacturer serving customers across motion control
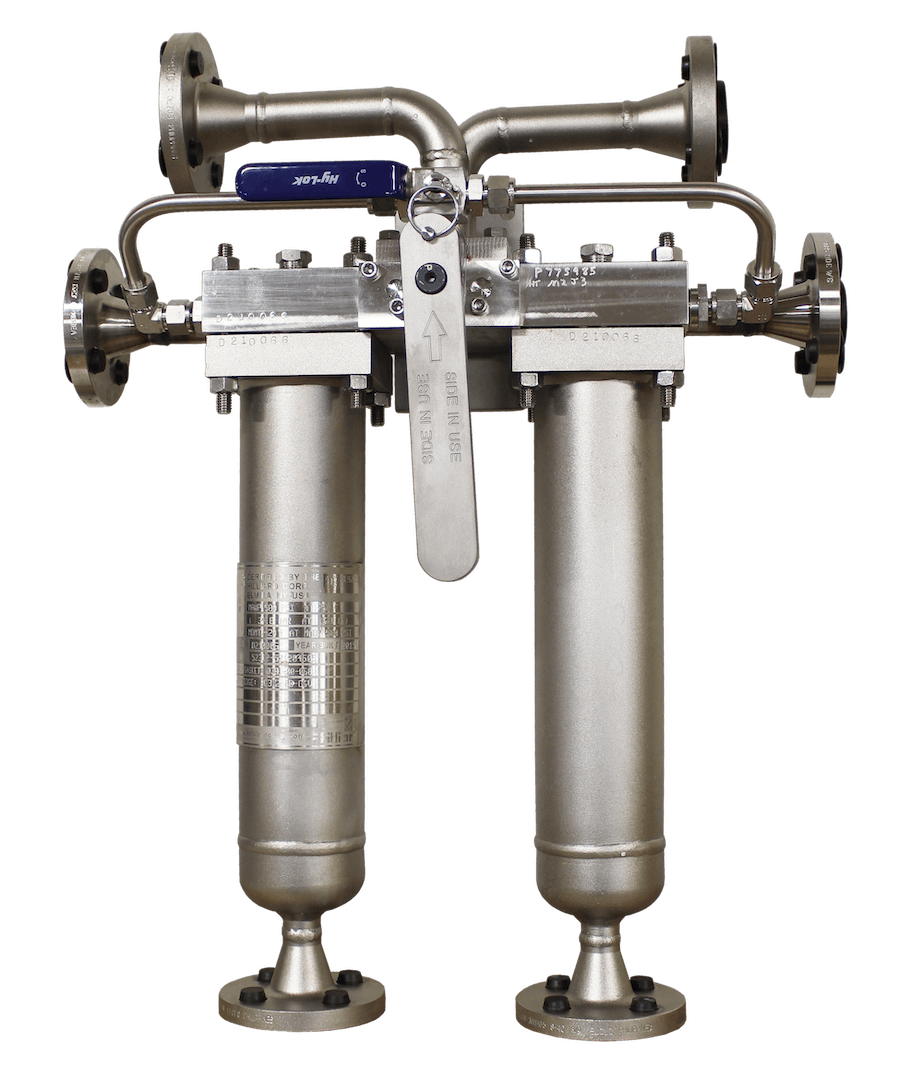
Filter Equipment
Complete filtration, separation, and fluid conditioning systems for industrial applications.
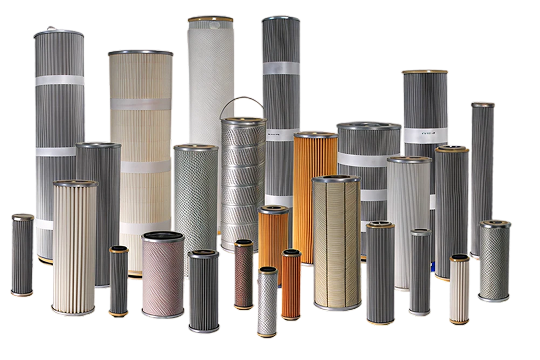
Filter Cartridges
High-performance filtration media for contamination control and fluid cleanliness.
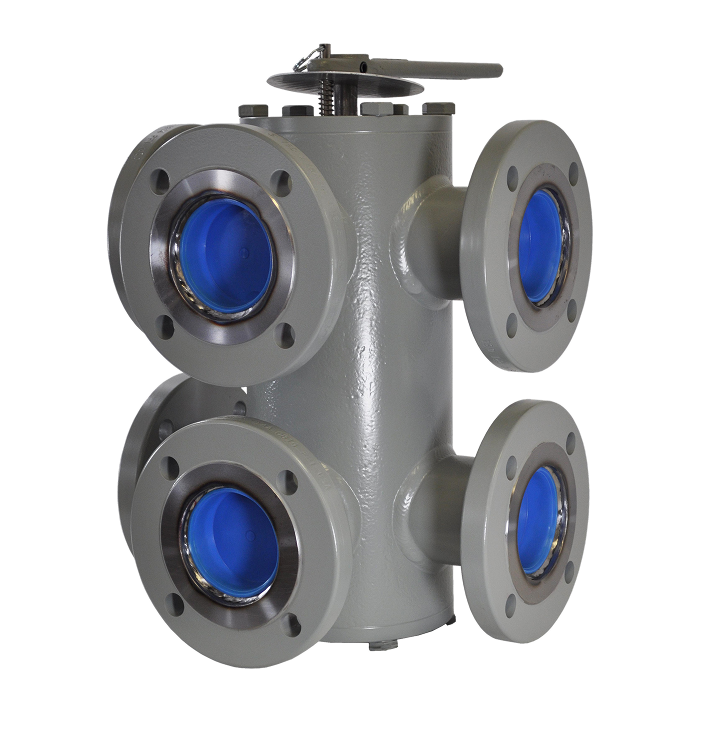
Valves
Industrial valve technologies for fluid isolation, flow diversion, and process control.
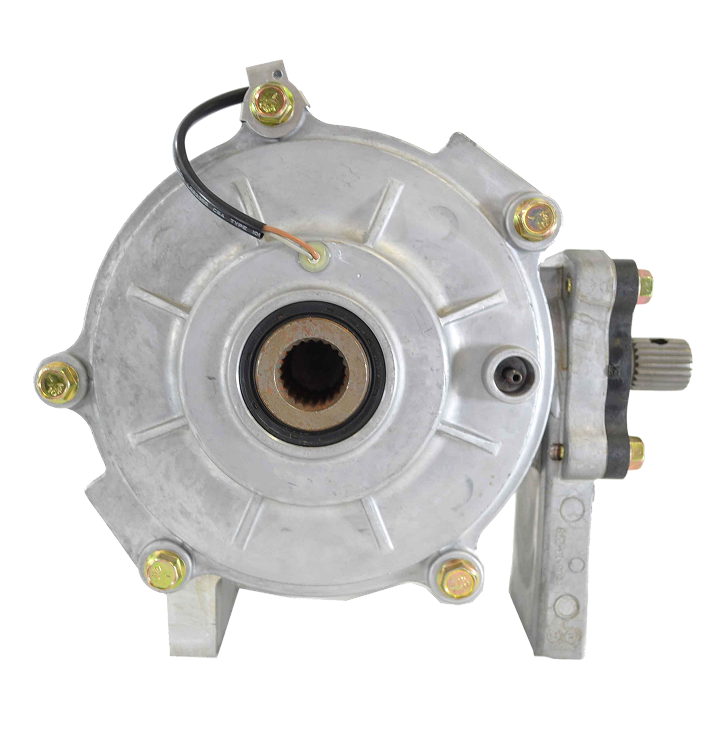
Drivetrain
Mechanical drivetrain systems for power transfer, traction control, and variable speed operation.
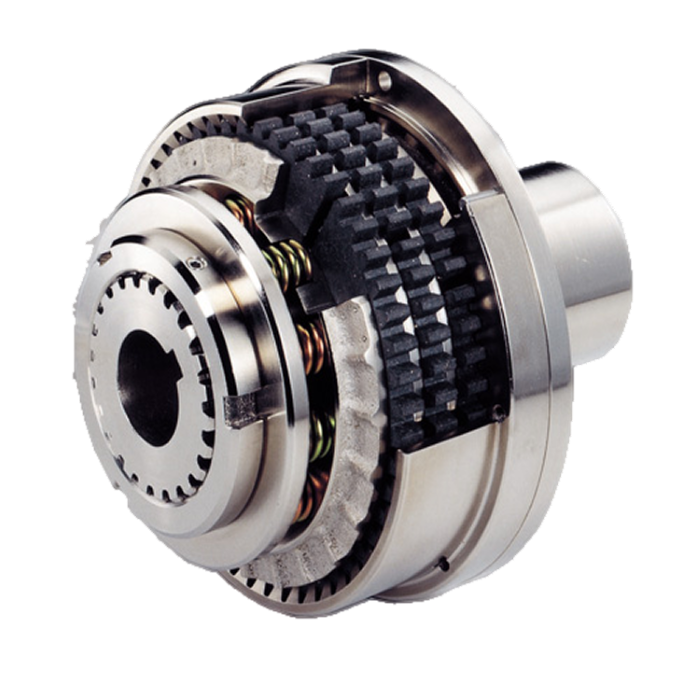
Motion Control
Clutch and torque limiting technologies for controlled power transmission and equipment protection.
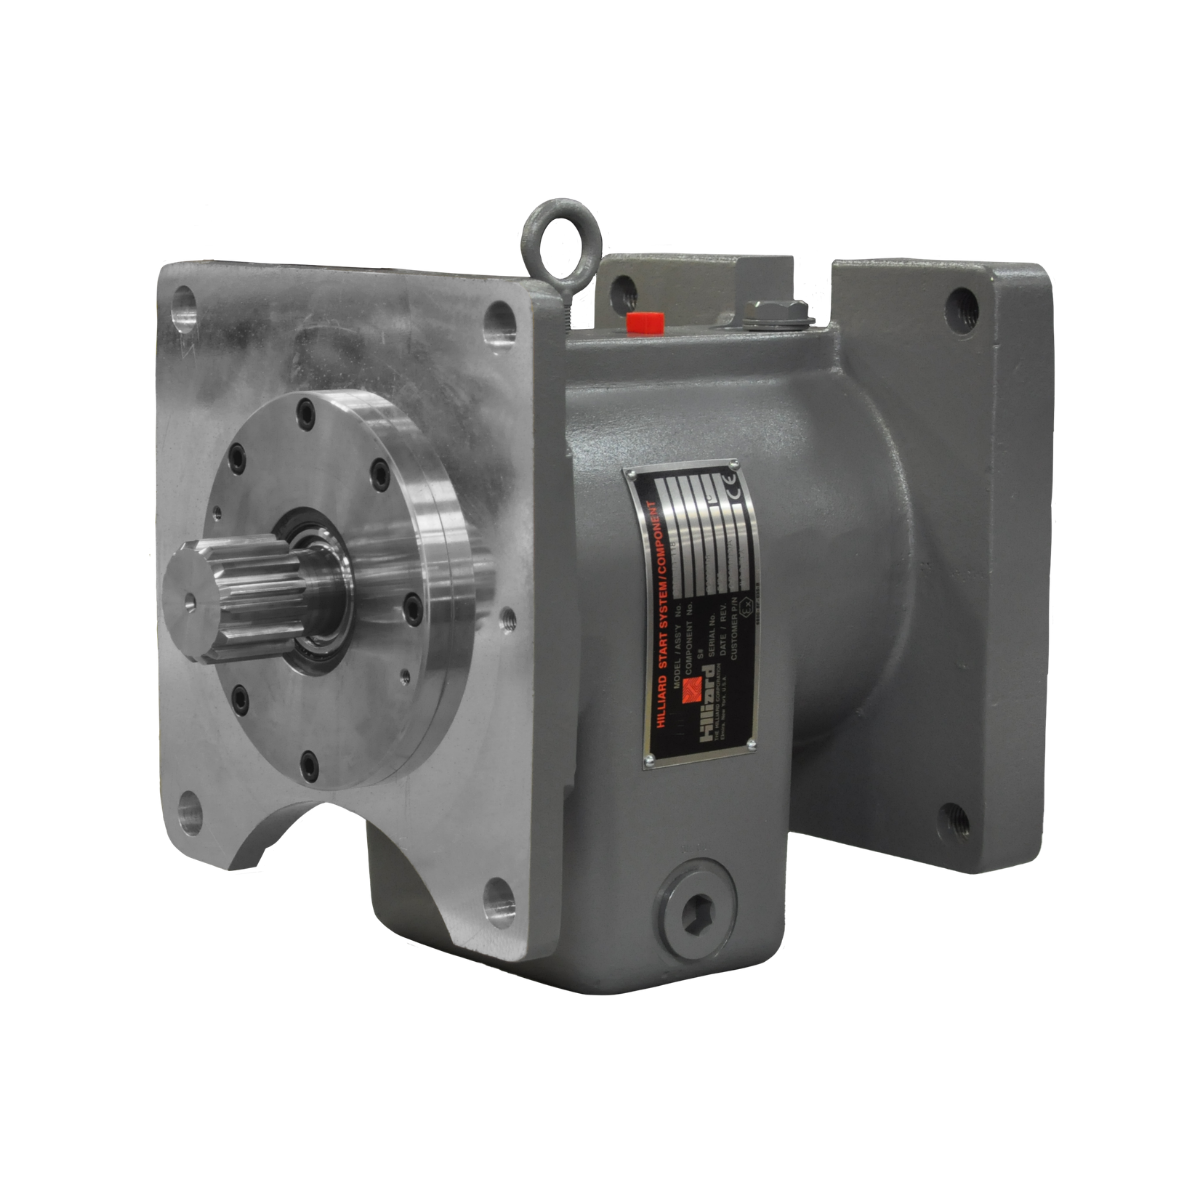
Engine Starters
Electric, hydraulic, and pneumatic starting systems for industrial engines and turbines.
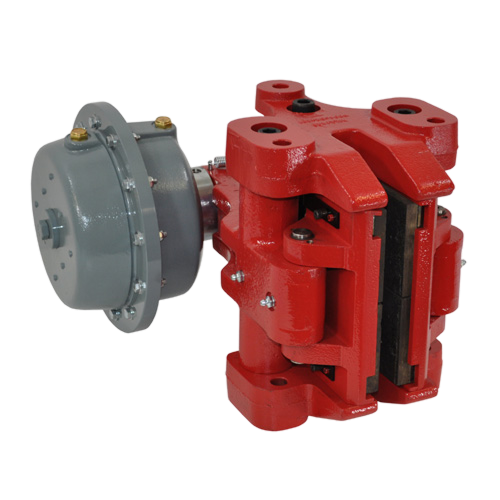
Industrial Braking Systems
Industrial braking technologies for stopping, holding, positioning, and controlled deceleration.
Application-Specific Filtration for Industrial Fluid Systems
Contamination Control
Fluid Cleanliness
Equipment Protection